

Capacity Is More Than a Number on a Machine
When investors begin planning a sawdust cat litter project, one of the first questions is usually: “What capacity should the line have?”
It sounds simple, but the answer depends on much more than the desired output.
A production target influences raw-material storage, milling, forming, drying, cooling, screening, packaging, electrical demand, labor and finished-product inventory.
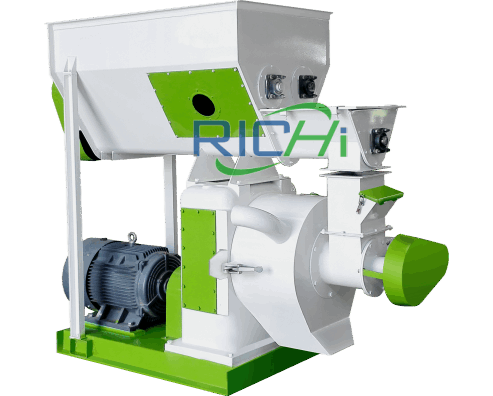
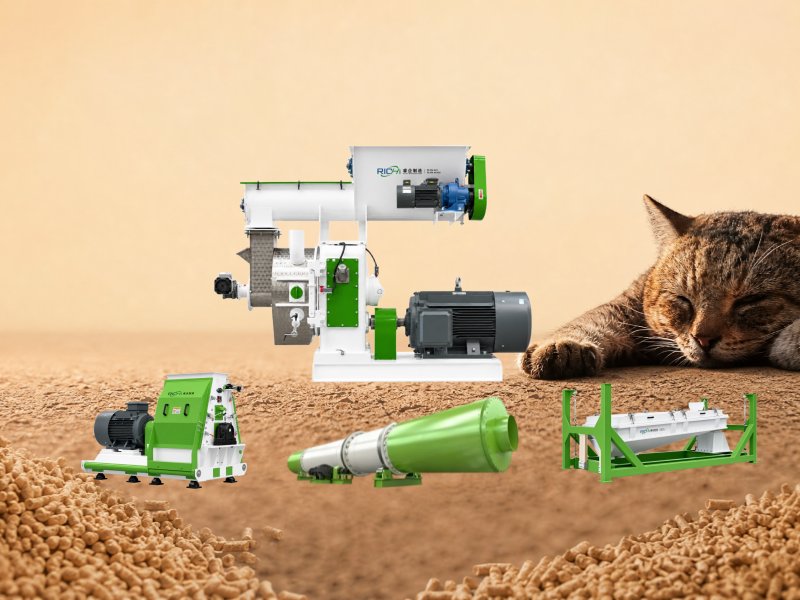
A line producing 1 T/H needs a very different material flow from a line designed for 5 T/H. At the same time, a sawdust cat litter making machine with a nominally high capacity may not achieve that output when handling a specific type of sawdust.
That is why project capacity should be treated as a system-design parameter.
Start With Available Raw Material
The first calculation should be based on how much usable material is available.
A factory may theoretically produce several tons of sawdust every day, but part of that material may already be sold to another customer or may have unsuitable moisture and contamination levels.
A better approach is to calculate:
Daily usable sawdust × operating hours × working days = practical monthly feedstock availability.
This immediately gives the project a more realistic production boundary.
For example, a factory with a limited and irregular raw-material supply may be better suited to a smaller line with flexible operating hours than a large automated installation.
Typical Capacity Planning Scenarios
There is no universal capacity for sawdust cat litter production, but several planning ranges can be used as project examples.
Small Commercial Production
A small system may be suitable for a new market entrant, a woodworking company or a regional pet-product manufacturer.
The priorities are often:
- Lower initial investment
- Compact layout
- Flexible operation
- Easy maintenance
- Ability to scale later
Medium Production
A medium-scale project may serve a dedicated pet-litter business or a larger wood-processing company.
The focus shifts toward:
- Continuous operation
- Balanced drying capacity
- Automated conveying
- Stable product quality
- Higher packaging efficiency
Large Industrial Production
Large projects require greater attention to process integration.
The production line may include automated feeding, central dust control, advanced electrical systems, larger drying sections and high-speed packaging.
At this scale, a bottleneck of only a few minutes per hour can create significant production losses.
Why Drying Capacity Often Determines the Real Output
The forming machine may appear to be the main production unit, but drying can become the actual limiting stage.
This is why manufacturers should evaluate an industrial sawdust dryer machine for sale according to the complete process rather than looking only at the advertised material throughput.
The dryer must handle the actual inlet moisture and deliver the target outlet condition at a stable rate.
For example, two plants with identical forming machines may need different dryers if their incoming sawdust has significantly different moisture levels.
Climate also matters.
A plant operating in a humid environment may deal with different storage and drying conditions from one located in a dry region.
Capacity Should Include Moisture Loss
Another common planning mistake is assuming that the weight of incoming sawdust is equal to the weight of finished litter.
It is not.
If moisture is removed during drying, the final mass will be lower than the initial wet feedstock weight.
Therefore, production calculations should distinguish between:
- Wet raw-material input
- Dry-matter input
- Water removed
- Final product output
- Screening losses
- Recycled material
This is especially important when estimating equipment capacity and operating cost.
How Particle Size Affects Throughput
Particle preparation influences machine feeding and forming behavior.
Material that is too coarse may reduce stable production, while excessive fine material can increase dust and create handling challenges.
The capacity calculation should therefore consider the condition of the feedstock entering the forming stage.
If the available sawdust contains many larger chips, additional milling may be required.
If the raw material is already fine and uniform, the preprocessing section can be simplified.
In other words, the same machine specification can behave differently depending on the material being processed.
Designing Around Future Expansion
Many investors want to know whether they should build a larger line immediately or start smaller.
A practical approach is to design the plant with expansion in mind.
For example:
- Leave space for additional dryers
- Install conveyors that can be extended
- Reserve electrical capacity
- Plan storage areas for future growth
- Use modular equipment where practical
- Keep the packaging area expandable
This can make future upgrades easier without requiring the entire production plant to be redesigned.
The Role of Automation at Different Capacities
Automation becomes increasingly valuable as production volume increases.
At smaller capacities, operators may manually monitor material flow and packaging.
As the plant becomes larger, automated control can help manage:
- Feed rate
- Dryer temperature
- Material flow
- Motor operation
- Alarm conditions
- Cooling
- Product transfer
The goal is not automation for its own sake.
The real purpose is to make the production process more stable and reduce unnecessary manual intervention.
Choosing Equipment as a Balanced System
A good production line should have reasonably balanced capacity between its major sections.
For example, there is little value in installing a high-capacity forming machine if the dryer cannot process the output.
Likewise, a high-capacity dryer does not create additional value if the raw-material preparation section cannot provide enough conditioned material.
This is where supplier experience becomes important.
A company such as Richi manufacture can evaluate the complete process flow and help match the equipment combination to the intended output, raw material and product specification.
The important point is to evaluate the entire system rather than one machine at a time.
Product Type Also Influences Capacity
Not every sawdust cat litter product has identical processing requirements.
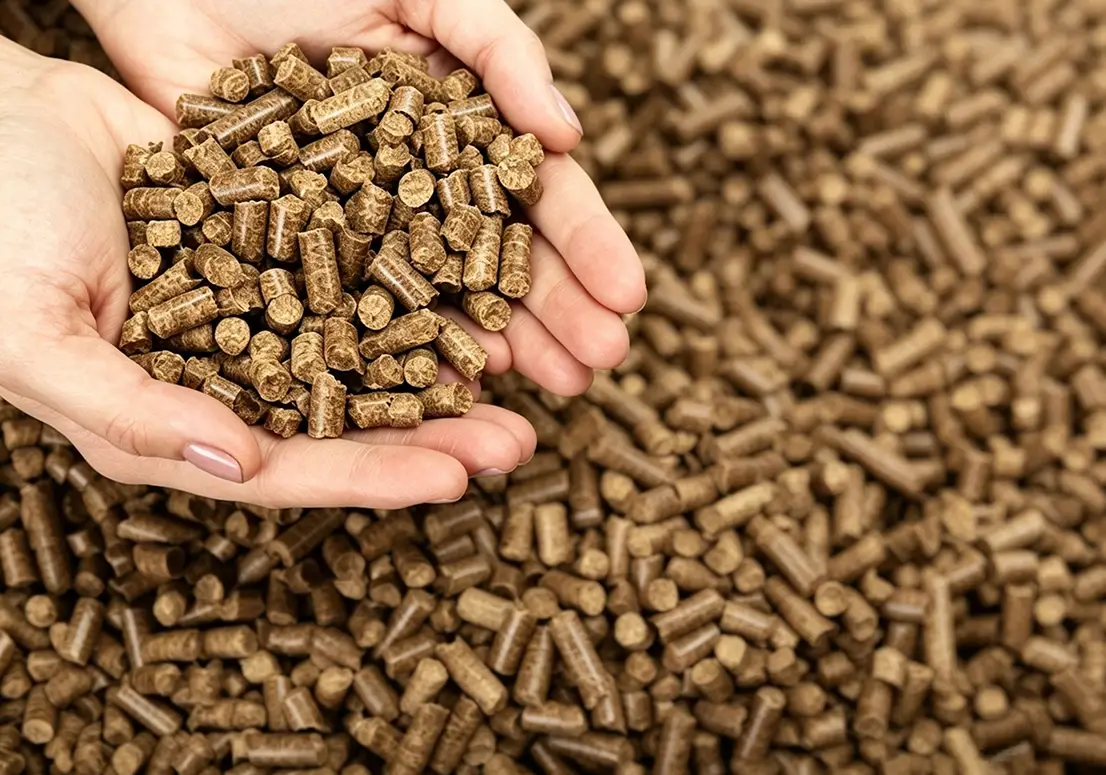
A manufacturer may produce lightweight litter, denser particles, larger granules or a product designed for specific packaging formats.
Different product specifications can affect:
- Forming conditions
- Drying demand
- Cooling time
- Screening
- Packaging speed
Therefore, capacity should be defined together with product specifications.
“5 T/H” is meaningful only when the material and product condition are also clearly defined.
What Does a Capacity Study Need to Include?
Before ordering equipment, investors should prepare a short project data sheet containing:
Raw material:
- Species
- Moisture
- Particle size
- Daily availability
Finished product:
- Particle dimensions
- Density target
- Moisture target
- Packaging format
Factory:
- Available floor space
- Electricity
- Heat source
- Working hours
- Storage capacity
Business:
- Planned monthly output
- Target markets
- Expected operating schedule
- Future expansion plan
With this information, equipment selection becomes much more precise.
Don’t Let the Largest Number Make the Decision
A larger machine does not automatically create a better business.
Oversized equipment can mean higher investment, more complicated operation and more unused capacity during the early stage of a project.
The better strategy is to match capacity to available raw materials and realistic market demand while preserving room for future expansion.
For anyone comparing sawdust processing technologies, find out here now for additional ideas on production planning and equipment selection.
Final Thought
Capacity planning should answer one question: how much product can the whole system produce consistently under real operating conditions?
That includes raw-material supply, milling, moisture control, forming, drying, cooling, screening and packaging.
Once these factors are understood, choosing the appropriate line capacity becomes a technical decision rather than a guess based on a machine brochure.