
A corn hammer mill should be selected by the particle-size distribution required by the next process, not simply by its maximum tonnes-per-hour rating. Corn can be ground into coarse particles for some feed applications or finer meal for mixing and pelleting. The screen, rotor, hammer condition and feed rate determine the actual result. A machine that produces high throughput at a coarse setting may deliver much less output when the customer requires a finer grind.
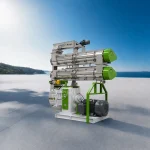
RICHI’s corn hammer mill page lists reference capacities of 3–50 t/h and main motor ratings of 37–220 kW, with adjustable particle sizes from 0.5 to 20 mm. The basic configuration uses gravity feeding, while the upgraded version adds a variable-frequency impeller feeder, permanent-magnet iron remover and pneumatic gate. The correct configuration depends on the plant’s receiving method, automation level, corn condition and downstream process.
Translate the Feed Formula Into a Grinding Specification
Before selecting the mill, list the feed products that will use the ground corn and define the required particle-size distribution for each. Mash feed, pellet feed and different poultry growth stages may not use the same grind. A target expressed only as a screen aperture is incomplete: the actual output also depends on corn moisture, kernel hardness, hammer wear, rotor speed and feed rate. Define the acceptable proportion of fines and coarse particles where product quality requires it.
If one mill serves several recipes, estimate how often the screen or operating setting will change. Frequent product changes may affect production scheduling and maintenance. If two particle-size ranges are required at the same time, compare the cost of separate grinding routes with the downtime and handling involved in repeated screen changes.
Corn condition should be checked at receiving. Moisture, broken kernels, foreign matter and storage deterioration can affect grinding performance. A pre-cleaning stage and magnetic separation help remove contaminants before they reach the rotor. If the corn supply varies by season or supplier, retain representative samples and record the operating settings associated with each batch.

Choose the Feeder Configuration for the Receiving System
A gravity-fed hammer mill can be suitable where the raw material is consistently delivered and the process is relatively simple. It has a straightforward layout and may reduce initial equipment cost. However, the receiving hopper and upstream conveyor must still provide a stable feed without surges. If material enters unevenly, motor load and particle-size consistency can fluctuate.
The upgraded configuration described by RICHI uses a variable-frequency impeller feeder, permanent-magnet iron remover and pneumatic gate. This arrangement is intended for more controlled feeding and continuous commercial operation. The feeder speed can be adjusted to match the mill load, while the magnet helps remove ferrous contaminants. The pneumatic gate supports controlled material entry and isolation.
The choice should reflect the labor model and operating hours. A small facility with limited throughput may prefer a simple system if operators can supervise feeding safely. A commercial plant running long shifts may benefit from automated feeding and interlocks. In either case, provide safe access to inspect the magnet and remove collected metal without reaching into moving equipment.
Select Screen and Hammer Arrangement for the Required Grind
The screen controls the size at which particles can leave the grinding chamber, while hammer condition and rotor speed influence the rate of size reduction. RICHI describes reversible high-manganese steel hammers that can be used on either side. This can extend usable service before replacement, but inspection is still necessary because uneven wear can affect balance and grinding performance.
The screen should be selected from the target particle size and the material’s grinding behavior. Smaller openings generally require more work to pass material through and may reduce throughput. A screen that is too coarse may produce particles unsuitable for the mixer or pellet mill. Confirm the result through a sample analysis rather than assuming the nominal screen opening equals the final particle size.
The rotor should be dynamically balanced and installed according to the equipment procedure. Abnormal vibration, noise or bearing temperature may indicate buildup, uneven hammer wear, loose fasteners or a mechanical problem. Stop and isolate the machine before inspection. Do not continue operating a hammer mill with abnormal vibration.
Integrate Dust Control and Explosion-Risk Management
Corn grinding generates dust, especially around the feed inlet, discharge, cyclone and transfer points. The page describes a mesh-clamping device intended to improve sealing and reduce dust escape. The complete dust-control system may include a cyclone, filter, fan, ductwork and a safe dust-discharge route. The required configuration should follow the plant’s risk assessment and applicable local standards.
Dust collection must be sized for the airflow and equipment arrangement. Poorly routed ducts, blocked filters or inadequate discharge can reduce capture performance. Provide inspection doors, filter replacement access and a cleaning schedule. Housekeeping should prevent dust layers from accumulating on beams, motors and cable trays.
The plant should review ignition sources, grounding, bearings, hot surfaces, tramp metal and safe isolation. Dust hazard controls depend on the material, building and local regulations; a dust collector alone does not establish that the installation is safe. The owner should obtain the appropriate engineering and safety review before commissioning.
Balance the Hammer Mill With the Rest of the Feed Line
A corn hammer mill may feed a mixer, batching system or pellet production line. Confirm the capacity of the discharge conveyor, elevator, storage bin and downstream equipment. If the mixer cannot accept the grinding rate, material will accumulate. If the grinder is undersized, the pellet mill may starve. Use the expected operating schedule and product mix to balance the process.
Check electrical requirements, motor starting, overload protection, cable routing, earthing and control signals. The mill should interlock with upstream feeding and downstream conveying. If the receiving bin is full or the downstream conveyor stops, the feeder should respond safely. Provide maintenance clearance for screen replacement, hammer inspection, rotor access and motor removal.
Validate Output With a Particle-Size Test
A production trial should use the customer’s normal corn supply. Record moisture, feed rate, screen size, rotor speed where adjustable, motor current, throughput and the resulting particle-size distribution. Take samples from a representative discharge point and use a consistent test method. Repeat the test after a screen change or major adjustment.
Acceptance criteria should state the required throughput and particle-size distribution, including the allowed coarse and fine fractions. If the mill is used for multiple recipes, test each important grind setting. A single high-output trial at a coarse setting should not be used to represent a finer grinding duty.
Corn Grinding Energy per Accepted Tonne
Compare grinding settings using metered electricity per tonne of corn that passes the agreed sieve test. During a stable run, record energy consumed, gross tonnes processed, accepted tonnes, rejected coarse fraction and recirculated material. Divide metered kilowatt-hours by accepted tonnes rather than gross intake. A finer screen may increase energy use and reduce throughput, but it may be necessary for downstream feed quality. The lowest energy figure is not the best setting if particle distribution fails the specification.
For example, if a test consumes 48 kWh while processing 4.0 tonnes, but only 3.7 tonnes meet the required distribution, the relevant figure is approximately 13.0 kWh per accepted tonne, not 12.0 kWh per gross tonne. Use the same measurement boundary and sieve method when comparing screens. Recalculate after changes in moisture, hammer condition, screen opening or downstream particle target. This gives procurement and production teams a consistent basis for comparing settings and estimating electricity cost per saleable tonne of feed.
Corn Hammer Mill Capacity Selection
Calculate daily accepted corn demand and divide it by realistic grinding hours after allowing for cleaning, screen changes and planned maintenance. Validate the hourly requirement with the selected screen and a representative corn sample. A capacity quoted at a coarse grind should not be transferred to a finer grind without a trial. If the mill supplies several formulas, include screen-change time in the production schedule and confirm the discharge conveyor, storage bin and mixer can accept the selected grinding rate.
For each approved product, record the corn lot, moisture, screen identification, hammer condition, feeder setting, motor current, run duration, sieve result and accepted tonnes. After screen or hammer maintenance, repeat the sieve test before returning to full production. Stop and isolate the machine before opening the grinding chamber or removing a screen. This record helps distinguish a change in raw material from mechanical wear and provides a defensible basis for deciding whether the mill needs a different screen, a revised schedule or additional capacity.
Receiving Inspection and Batch Traceability
At receiving, inspect corn for moisture, broken kernels, mold damage, stones, metal and other foreign material. Record supplier, delivery lot, net weight and inspection result. Magnetic separation captures ferrous contaminants but does not remove stones or non-metal objects. Keep lots identifiable until acceptance checks are complete, and link the grinding record to the mixer batch. If a particle-size sample fails, hold the ground corn and investigate screen seating, hammer wear, feed consistency and possible bypass before it enters the formula.
Where the mill is connected to automated batching, verify that the correct ground-corn bin is selected for each recipe and that high-level and low-level signals function correctly. Prevent cross-contamination between grind grades by defining bin assignment, transfer routing and cleanout responsibility. Include these checks in commissioning and operator training. Retain a sample from each approved grind so that production staff can compare later results against a known reference rather than relying on visual judgment alone.
Conclusion: Specify the Grind Before Comparing Hammer Mills
The right corn hammer mill is the one that produces the required particle distribution at the plant’s expected operating rate while fitting the receiving, dust-control and downstream systems. Feeder design, screen selection, hammer condition, rotor balance and maintenance access all influence the result. Compare proposals using the same corn condition and grinding specification.
For model options and configuration details, review the RICHI corn hammer mill range. Prepare corn samples, moisture data, required particle-size distribution, target throughput, operating hours and site utility information before finalizing the model.